
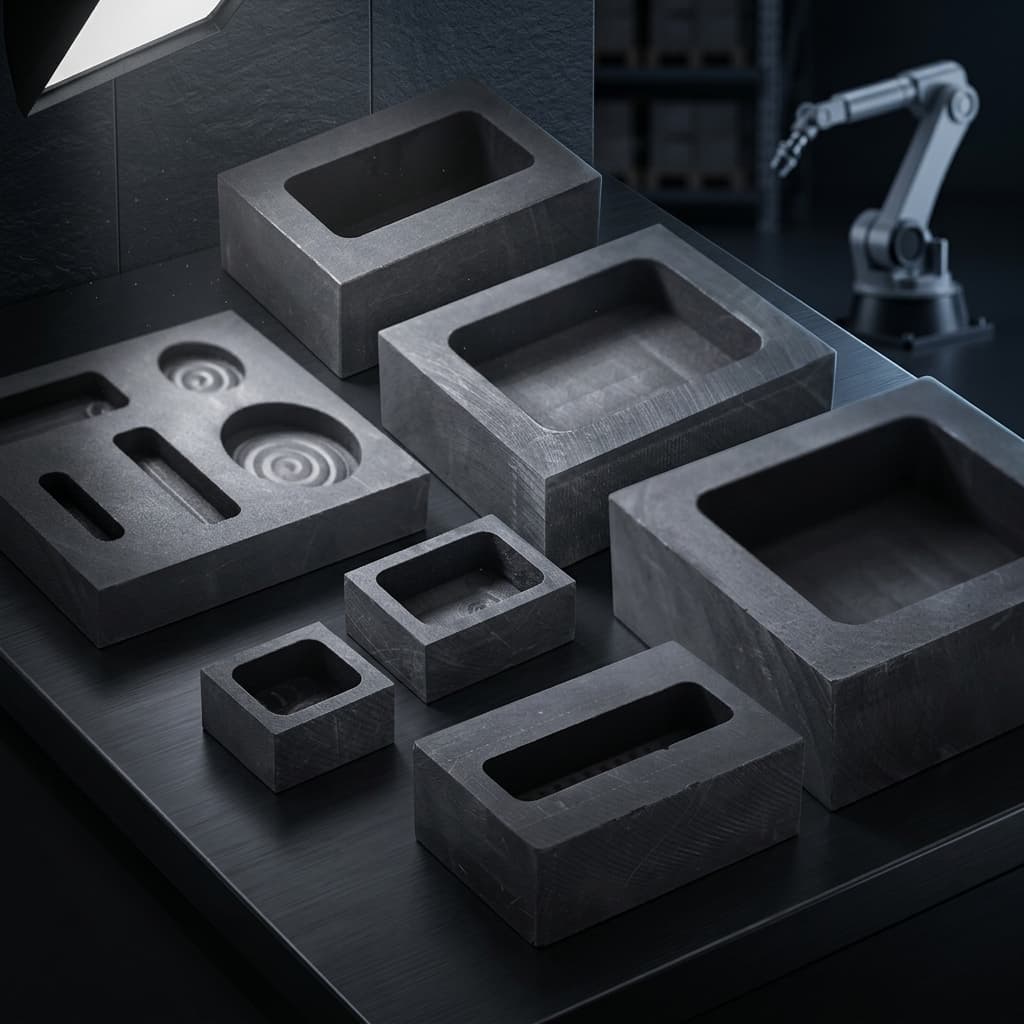
3D Glass Hot Bending Graphite Molds: Ultrafine Grain Selection, CTE Thermal Mismatch, Surface Mirror Polish (Ra ≤ 0.2 µm) & Lifespan Sourcing Guide
Specify 3D glass hot bending graphite molds: compare grain grades, CTE mismatch, Ra ≤ 0.2 µm finish and lifespan evidence. Prepare your drawing for an RFQ review.
Selection answer: Specify 3D glass hot bending graphite molds against the exact glass grade, furnace cycle, contact geometry and acceptance method. Ultrafine isostatic graphite is a candidate for glass-contact surfaces, but grain size alone cannot establish optical quality. Treat Ra ≤ 0.2 µm as a drawing requirement to verify on a finished sample. Calculate differential thermal expansion for clearance screening, then establish contour compensation and useful mold life through forming trials with defined rejection limits.
Published and reviewed: November 10, 2026. This English-language guide serves global glass-forming engineers, tooling designers and procurement teams sourcing custom graphite cavities, punches and carrier frames. It covers heated forming of curved cover and display glass; it does not specify a validated recipe for optical lenses, ultra-thin foldable glass or a particular branded glass formulation.
Evidence and limits: The standards cited below support measurement methods. The worked calculations use explicitly assumed inputs; the sourcing tables are decision aids, not measured grade benchmarks. This article contains no factory trial dataset, independently verified service-life result or customer case study. Product images and the schematic illustrate tooling concepts and do not certify finish, dimensions or manufacturing capability.
A useful RFQ connects four decisions: which material can retain the required surface, how the glass and tooling move during heating, what constitutes an acceptable formed panel, and when the mold should be refurbished or retired. Buying solely on a graphite grade name or a promised cycle count leaves these questions unresolved.
Already defining a tooling program? Request a drawing and process review with your glass datasheet, STEP model, furnace atmosphere and acceptance criteria. For tooling configurations, start with the 3D glass graphite molds product overview.
1. Operating Mechanics: 3D Glass Hot Bending & Tooling Demands
Glass does not have one universal forming temperature. Its viscosity changes with temperature and composition, while thickness, load and dwell time determine how quickly a blank deforms. A supplier's softening-point value is a material characterization result, not an instruction to operate a production furnace at that temperature. ASTM C338 describes a glass softening-point test; it does not qualify a complete hot-bending cycle.
Distinguish the softening point from the annealing and strain regions. These describe different aspects of glass behavior. Obtain the glass producer's viscosity-temperature and thermal-expansion data for the supplied grade, and ask whether forming occurs before or after chemical strengthening. Do not transfer a recipe between aluminosilicate and soda-lime glass on the basis of a family name.
Three forming approaches impose different tooling requirements:
- Gravity sagging: The blank deforms under its own weight. Support locations and dwell time influence the contour; limited contact may reduce surface transfer in some designs.
- Vacuum-assisted forming: Pressure difference helps bring glass toward the cavity. Vent layout, sealing and local contact sequence can determine whether trapped gas or vent impressions remain.
- Punch-and-cavity pressing: Opposed surfaces control more of the shape. The stack needs a defined hot gap, alignment strategy and load distribution to avoid local overloading.
A pressure value is incomplete without the loaded area and machine control mode. Likewise, a furnace temperature is incomplete without the mold temperature history. Record heating, dwell and cooling conditions together rather than comparing isolated setpoints.
Concept schematic, not to scale. Vent dimensions, hot clearances and atmosphere limits must be established for the selected glass and machine.
Why Isostatic Graphite Is a Candidate
Isostatic graphite offers machinability, thermal-shock resistance and grades with relatively low thermal expansion. These properties make it useful for complex mold geometries. They do not guarantee release, zero contamination or identical temperature response across a large panel. Glass chemistry, surface condition and atmosphere remain part of material qualification.
Metallic and ceramic tooling should be assessed against their own thermal expansion, release behavior and surface treatments. A blanket claim that all metal molds fail is not a sound purchasing rule. Compare finished-glass results and total cost under the same process conditions before approving a material substitution.
2. Thermal Expansion Physics: CTE Mismatch & CAD Shrinkage Compensation
Start with the reference temperature, nominal dimensions and the meaning of each quoted coefficient of thermal expansion (CTE). A room-temperature datasheet value cannot automatically be extended through the glass transition or across the entire furnace cycle. ASTM E228-22 addresses push-rod measurement of expansion in rigid solids; it does not establish how softened glass flows or springs back.
For a first-order clearance screen using constant mean coefficients:
ΔT = evaluation temperature − reference temperature
ΔL_mold = L0 × α_mold × ΔT
ΔL_glass = L0 × α_glass × ΔT
ΔL_diff = L0 × (α_glass − α_mold) × ΔT
Use millimeters for L0, kelvins for ΔT, and per-kelvin units for CTE. This model assumes uniform temperatures, free expansion and constant mean properties. For design work, use validated temperature-dependent expansion data over the relevant interval and account for thermal gradients and constraints.
Reproducible Clearance Example
Assume a 160 mm reference length at 25°C, evaluated at 720°C. For illustration only, choose mean CTEs of 4.6 × 10⁻⁶/K for graphite and 8.5 × 10⁻⁶/K for glass. These are calculation inputs, not certified properties of a specified grade.
ΔT = 720 − 25 = 695 K
Mold growth  = 160 × 4.6 × 10⁻⁶ × 695 = 0.51152 mm
Glass growth = 160 × 8.5 × 10⁻⁶ × 695 = 0.94520 mm
Difference   = 0.94520 − 0.51152 = 0.43368 mm
For a symmetric pocket around a centered blank, this idealized difference corresponds to approximately 0.217 mm per side before considering initial clearance, dimensional uncertainty and constraints. For a blank located against one fixed edge, the distribution is different. The result is not an automatic CAD scale factor or a predicted finished radius.
Table 1: Hypothetical Differential-Expansion Screen
All six rows use the same assumed CTEs above and a 25°C reference. Results are rounded only after calculation. Size labels indicate examples, not validated application recipes.
| Example reference length | Evaluation temperature | ΔT | Mold growth | Glass growth | Differential growth |
|---|---|---|---|---|---|
| 45 mm | 700°C | 675 K | 0.140 mm | 0.258 mm | 0.118 mm |
| 160 mm | 720°C | 695 K | 0.512 mm | 0.945 mm | 0.434 mm |
| 180 mm | 680°C | 655 K | 0.542 mm | 1.002 mm | 0.460 mm |
| 350 mm | 740°C | 715 K | 1.151 mm | 2.127 mm | 0.976 mm |
| 600 mm | 750°C | 725 K | 2.001 mm | 3.698 mm | 1.697 mm |
| 1,200 mm | 760°C | 735 K | 4.057 mm | 7.497 mm | 3.440 mm |
Clearance screening addresses possible interference during heating. Final contour compensation addresses a different question: what mold shape produces acceptable cooled glass after the actual forming and cooling sequence? Solve that through trial parts, measured deviations and controlled CAD revisions. Do not apply a universal over-bend percentage, a fixed per-100-mm clearance or a single shrinkage multiplier to every geometry.
3. Grain Structure & Optical Surface Replicability (Ra ≤ 0.2 µm)
Grain pullout, open pores, machining marks and local scratches can transfer defects to contacted glass. Ultrafine isostatic graphite may help achieve a more consistent surface, but grain size, crystallite size and pore size are different quantities. Require the supplier to identify what its reported particle-size number measures and how it was obtained.
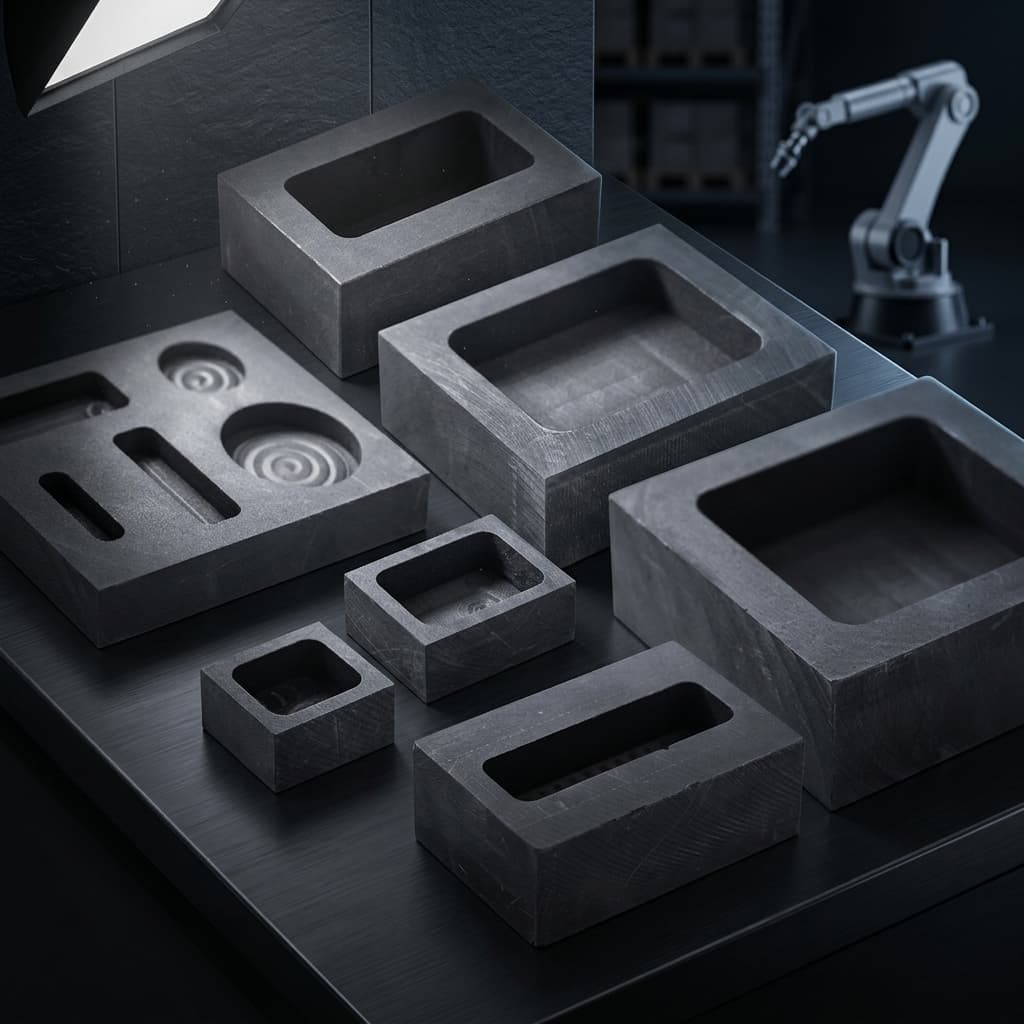
Tooling illustration only; the image does not demonstrate a measured Ra value or an accepted glass surface.
A request for a candidate grade in the 1–4 µm particle-size range can begin a supplier discussion, provided the supplier uses a comparable definition. It is not a universal acceptance threshold. Approve the material using a representative machined and polished coupon, followed by a forming sample with the actual glass.
Density, flexural strength and impurity content provide additional screening information. None individually proves low surface porosity, release performance or final optical quality. Ask for the grade name, production route, material-lot traceability, property test methods and any changes caused by purification or impregnation. ASTM C651-20 measures room-temperature four-point flexural strength; its result is not a hot-service load rating for a complete mold.
Make the Surface Requirement Measurable
A drawing note such as Ra ≤ 0.2 µm on designated glass-contact zones needs an agreed inspection procedure. Specify instrument type, filtering, evaluation length, measurement direction, accessible locations and the surface state at inspection. If an areal optical instrument is used, agree its reported parameters; Sa and Ra are not interchangeable labels.
Roughness also does not establish contour accuracy, waviness, scratch freedom or acceptable haze. Define these separately, with a reference sample or a stated optical inspection method where appropriate. A low average roughness can conceal an isolated pit that still rejects the glass.
Use a controlled machining and polishing sequence: retain finishing allowance, remove tool marks without rounding critical edges, clean away abrasive residues and inspect again. Polishing compounds and cleaning methods must be compatible with the surface treatment. Abrasive blasting is not a default final step for an optical-contact cavity. Ask whether the quoted finish applies before or after coating and final cleaning.
4. Material Grade Comparison for 3D Glass Hot Bending Molds
The following table compares qualification questions rather than assigning unsupported strength, temperature or service-life ranges to entire material families. Use the isostatic graphite materials overview to frame the material discussion, then request a grade-specific datasheet and sample evidence.
Table 2: Six Tooling Options and Their Qualification Gates
| Candidate | Possible role | Main selection issue | Evidence to request |
|---|---|---|---|
| Ultrafine isostatic graphite | Optical-contact cavity or punch | Pullout, pores and finish consistency | Polished coupon, surface map and formed-glass inspection |
| Fine-grain isostatic graphite | Less demanding contact zones | Whether finish meets the actual optical requirement | Grade definition and a trial against the same acceptance sample |
| Medium-grain isostatic graphite | Carrier or non-contact support | Strength, alignment wear and thermal movement | Assembly checks and thermal-cycle dimensional records |
| Anti-oxidation impregnated graphite | Candidate where oxidation limits life | Glass compatibility, residues and treatment uniformity | Treatment identity, contamination checks and comparative trials |
| CVD SiC-coated graphite | Candidate protective surface | Coating stress, pinholes, finish and dimensional buildup | Coating specification, thickness map and post-coating trial |
| Qualified carbon-based protective coating | Specialized surface option | Actual coating chemistry and release behavior | Named coating process, adhesion evidence and glass-contact trial |
A coating changes the contact surface and may change clearances. Obtain a finished, coated inspection result rather than accepting the uncoated substrate report. Pyrolytic carbon and glassy carbon are different material descriptions; an unspecified “carbon coating” is insufficient for ordering interchangeable tools.
5. Oxidation Degradation & Lifespan Sourcing
Graphite durability depends strongly on atmosphere and temperature. Oxygen ingress, moisture, thermal cycling, contact wear and handling damage can all contribute to retirement. There is no single oxygen threshold or onset temperature that guarantees acceptable life for every grade, coating and cycle.
An oxygen reading is useful only with its measurement location, calibration, sampling response and operating state. Record loading and unloading transients as well as steady-state dwell conditions. Nitrogen supply purity alone does not describe the atmosphere at the mold surface. Agree operating limits with the furnace and tooling suppliers, then validate those limits during the trial.
Compare Protection Routes Without Assuming a Cycle Guarantee
- Uncoated graphite: Avoids coating buildup and makes the base material's behavior easier to evaluate. It still needs a qualified atmosphere and a surface-wear inspection plan.
- Anti-oxidation impregnation: May reduce oxidation for a compatible formulation. Require evidence for the specific treatment and glass; do not assume every phosphate or silica treatment is suitable for an optical-contact face.
- CVD SiC coating: Can provide a protective barrier, but defects, edges, thermal stresses and glass interactions remain qualification issues. It does not make a mold immune to oxidation or handling damage. Include coating thickness and subsequent finishing in dimensional acceptance.
Define useful life as cycles until a stated rejection condition under a documented process. Possible limits include contour drift, unacceptable pits, rising glass reject rate, coating damage or loss of safe assembly clearance. Record repairs and re-polishing separately; a refurbished tool and a new tool are different lifecycle states.
For cost comparison, calculate:
Tooling cost per accepted panel =
(tool purchase + qualification + refurbishment + allocated tooling downtime)
÷ number of accepted panels produced
Use equivalent process conditions and include mold-related scrap consistently. Without comparable records, a supplier's “2,500 cycles” statement is an unqualified claim. Request the glass grade, temperature profile, atmosphere, inspection interval, sample size and failure definition before using it in a budget. No specific cycle-life range is established by the references in this article.
If the protection route is unresolved, send the proposed grade, atmosphere limits and acceptance plan for review before ordering a production set.
6. Tooling Architecture, Micro-Venting & Parting Line Design
A stack may include a lower cavity, upper punch and separate carrier or locating frame. Identify which surfaces contact the glass, which locate it during heating, and which remain loaded during cooling. A room-temperature assembly that fits well can still bind when its members expand at different rates.
Design vent paths around the contact sequence and optical viewing area. A hole large enough to evacuate gas may leave an imprint; a smaller one may clog or restrict evacuation. Establish vent diameter, edge condition and placement through a representative forming trial rather than applying a universal micro-hole size. Check vent continuity after surface treatment and cleaning.
Specify the hot gap and demolding path with the glass thickness distribution, press behavior and datum strategy. Draft, edge radii and cold clearance require geometry-specific review. Avoid assuming that one draft angle or a standard room-temperature pin fit guarantees release throughout the cycle.
Inspection should connect the tooling CAD model to an agreed datum system. Request a map of profile deviation, accessible surface measurements, alignment checks and clearly stated measurement uncertainty. Large freeform surfaces need a sampling plan; a single best-fit average can hide local errors in critical viewing zones.
7. Troubleshooting Matrix: Root Causes & Engineering Controls
Use this matrix to organize investigation. The listed causes are possibilities, not a diagnosis. Change one controlled variable at a time and preserve the original process record so that a corrective action can be evaluated.
| Observed defect | Possible tooling or process contributor | First check | Controlled next step |
|---|---|---|---|
| Haze or orange peel | Surface pits, residues or contact conditions | Compare mold and glass surface maps with cleaning history | Trial a qualified finish or cleaning change on one tool |
| Incomplete curvature or local hollows | Trapped gas, uneven heating or insufficient dwell | Check vent continuity and measured mold temperatures | Adjust venting or the cycle within the approved trial plan |
| Perimeter chipping | Edge interference, handling damage or cooling stress | Inspect incoming blanks and evaluate hot-clearance assumptions | Revise locating clearance or handling after confirming the cause |
| Black particles or smudges | Machining dust, oxidation, residues or abrasion | Inspect particle source, tool condition and atmosphere logs | Correct the identified contamination path and inspect trial glass |
| Cooled contour error | Temperature gradients, restraint or compensation error | Compare cooled-part scans using fixed datums | Revise contour or process settings with a documented trial |
| Uneven press contact | Alignment drift, gap variation or stack interference | Inspect assembly, contact distribution and hot movement | Correct alignment or the load sequence before further trials |
Black marks are not proof of oxidation by themselves. Similarly, an out-of-profile panel does not prove that a graphite grade is unsuitable. Inspect the glass batch, furnace conditions and tooling together before buying a replacement material.
8. Sourcing & RFQ Engineering Checklist
Use this checklist to make quotations comparable. Mark unknown inputs explicitly and assign responsibility for resolving them before production approval.
- Controlled geometry: Supply the finished-glass drawing and STEP model, revision, reference temperature and a separate tooling model if available. State who owns thermal and contour compensation.
- Glass identity: Include exact grade, supplier, thickness, initial condition and the producer's forming and expansion data. Identify the chemical-strengthening sequence.
- Process envelope: Record forming method, temperature history, dwell, cooling sequence, applied load or vacuum and the machine's operating limits.
- Atmosphere evidence: Describe gas supply, oxygen and moisture monitoring, sensor location, transients and agreed alarm response.
- Material traceability: Ask for graphite grade, lot identification, particle-size definition, test methods and relevant property data over the applicable temperature range.
- Surface acceptance: Mark optical-contact zones and define roughness inspection, profile limits, scratch and pit criteria, contamination limits and the formed-glass reference.
- Treatment specification: Identify coating or impregnation chemistry, coverage, thickness where applicable, compatibility evidence and inspection after treatment.
- Venting and assembly: Include vent maps, datum references, pin and frame details, intended hot clearance and maintenance access.
- Trial and life protocol: Agree trial quantity, sampling intervals, rejection criteria, data ownership, refurbishment rules and the conditions of any life claim.
- Commercial handoff: State quantity, spares, lead-time requirements, destination, protective packaging, inspection deliverables and responsibility for nonconforming trial results.
For a broader tooling discussion, the custom graphite molds sourcing page is the relevant starting point. Process teams can also review the 3D glass hot bending solution overview alongside their furnace-specific documentation.
9. Frequently Asked Questions
Does Ra ≤ 0.2 µm guarantee a mirror-quality glass panel?
No. It is one mold-surface criterion. Waviness, pits, scratches, contamination, glass chemistry and the contact cycle can still affect the formed surface. Agree the mold measurement method and a separate finished-glass optical acceptance method. “Mirror polish” without these definitions is not a complete specification.
How many times can a graphite mold be re-polished?
There is no universal number. Measure material removal and inspect the resulting contour, edges, gaps and coating condition after each refurbishment. Retire or rework the tool when it cannot meet its drawing and formed-glass acceptance limits. Do not assume that two or three polishing operations are always available.
Can aluminosilicate and soda-lime glass use the same mold?
Possibly, but a shared nominal shape is insufficient evidence. Compare expansion data, viscosity behavior, release compatibility, glass thickness and the forming cycle. Repeat clearance review and formed-part inspection before approving a change of glass formulation.
What oxygen limit and nitrogen flow should the RFQ specify?
Use limits established by furnace qualification and the tooling trial. Flow depends on chamber design, leakage, loading and gas delivery, so one flow value cannot cover all machines. Include monitoring location, transient limits and the actions required when the atmosphere departs from the approved envelope.
Can a damaged SiC-coated cavity be repaired?
Ask the coating supplier to assess the actual damage. A small polishable surface mark differs from a coating breach or delamination. Stripping, recoating or replacement may be necessary, and each can affect dimensions and lead time. Do not accept an unverified local patch as equivalent to a qualified coating.
How should molds be cleaned between shifts?
Follow the approved procedure for the graphite grade and treatment. Remove loose particles without damaging contact surfaces, inspect vents and confirm dryness before reheating. Cleaning liquids can be retained in pores, and ultrasonic cleaning can damage some finishes or coatings. Solvent use requires equipment approved for that solvent; do not assume a general-purpose ultrasonic tank is suitable for flammable liquids.
Can one supplier guarantee finished-glass tolerances from mold machining data?
A mold inspection report establishes only the inspected tool condition. Finished-glass geometry depends on the full forming and cooling process. Define tooling tolerances and part tolerances separately, and require trial-panel measurements before approving production capability, especially on large curved displays.
10. Standards & References
These references support the named measurement methods, not the illustrative CTE inputs, supplier capabilities, coating compatibility or mold cycle life. Confirm the contractual edition and obtain the full method before writing an inspection specification. Public summaries are not substitutes for the standards.
- ASTM E228-22 — thermal-expansion measurement: Push-rod dilatometry for rigid solids; relevant to documenting CTE test conditions. It does not model softened-glass flow.
- ASTM C338-93(2019) — glass softening-point measurement: A material characterization reference, not a production furnace recipe. Automated access to this legacy catalogue URL was restricted during this review; confirm availability and the required edition with ASTM.
- ASTM C651-20 — graphite flexural-strength measurement: Room-temperature four-point bending of carbon and graphite specimens; not proof of a mold assembly's hot-service strength.
11. Engineering Support & RFQ Consultation
A useful sourcing decision ends with a documented qualification plan. Choose a candidate grade and surface route, resolve the clearance assumptions, approve a representative sample and retain the process data needed to evaluate service life. This sequence makes a low-priced mold and a premium coated mold comparable on accepted output rather than unsupported headline figures.
Contact Custom Graphite Parts for an RFQ review with your glass specification, 2D drawing, STEP model, annual demand and furnace conditions. Ask the quotation to identify proposed material, surface-treatment scope, inspection deliverables, trial responsibilities and confirmed lead time. Capability, attainable tolerances and any service-life commitment should be established for your project in the written offer.
Author
Graphite CNC machining, EDM electrode, mold tooling, and export-aware sourcing specialists.
More Posts
Resin-Impregnated vs. Antimony-Impregnated Carbon-Graphite for Mechanical Seals and Pump Bearings: Engineering Selection & RFQ Guide
Compare resin vs antimony impregnated graphite for seals and pump bearings. Check grade data, blistering risks and service limits, then prepare a complete RFQ.
Graphite CNC Machining Design Guide: Tolerances, Threads, and Cost Drivers
Designing custom graphite parts? Read our CNC machining guide covering standard tolerances, threading considerations, wall thickness limits, and tips to reduce your manufacturing costs.
Carbon-Carbon (C/C) Composites vs. Isostatic Graphite: Vacuum Furnace Fixture Selection Guide
Compare C/C composites vs isostatic graphite for vacuum furnace fixtures: thermal mass, TCO, risks, checklist, and RFQ guidance from Custom Graphite Parts.